
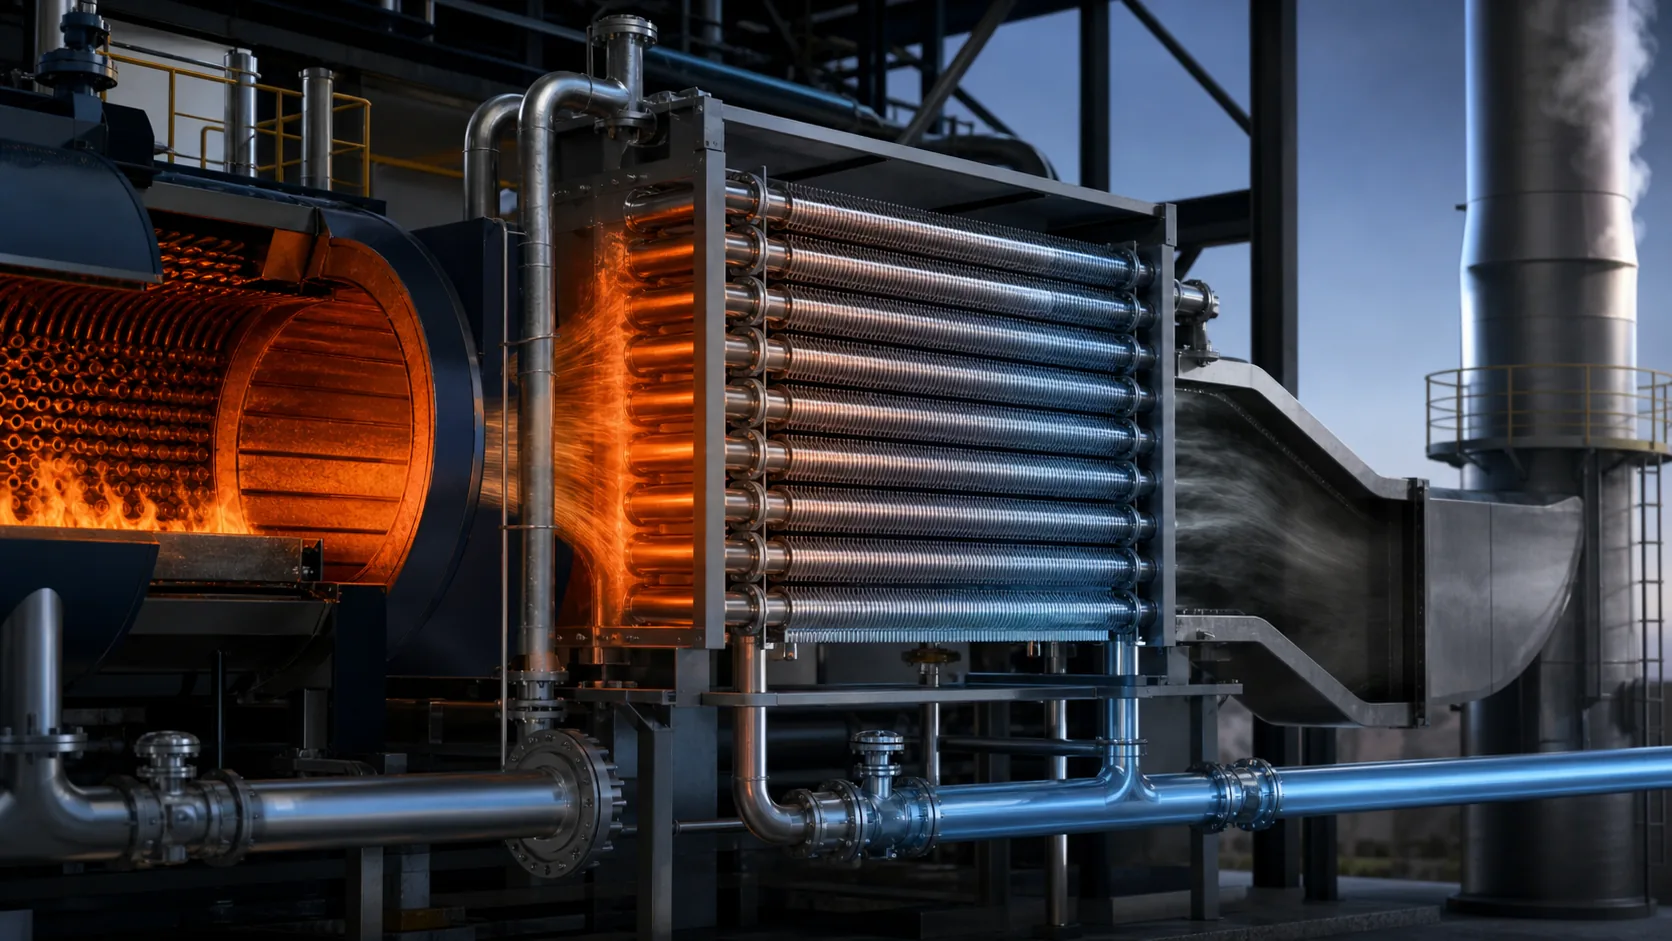
The economizer transfers the energy of the hot flue gas coming out of the boiler to feed water or another suitable fluid. Since the feed water enters the boiler hotter, the fuel required to produce the same amount of steam may decrease. However, there is no single savings percentage valid for every facility.
Real earnings; It is determined by the inlet and safe outlet temperature of the flue gas, water flow rate, operating hours, boiler load, fuel composition and current system efficiency. For this reason, the economizer decision should be made based on energy balance and corrosion control, not on the ratio in the catalogue.
How does the economizer work?
The flue gas at the boiler outlet cools as it passes through the heat transfer surfaces of the economizer. The feed water or process water inside the pipes is heated by receiving this energy. The boiler consumes less energy to raise the water to evaporation temperature.
Soot and ash loads in solid fuel facilities may require different surface and cleaning approaches compared to gas fuel facilities. Hisarmak’s solid fuel boiler economizer requires these conditions to be evaluated together with the fuel and ash character.
Variables that determine savings
Flue gas temperature
As the inlet temperature increases, the theoretical recovery potential increases. However, a high value may also indicate dirty surfaces, too much air or incorrect boiler settings. First, it should be verified that the existing boiler is working properly.
Feed water temperature and flow rate
Cold water can absorb more heat; However, in boiler systems, feed water may already be hot due to condensate return and deaerator. The water side flow rate of the economizer must be compatible with the boiler load.
Annual working hours
High clock and stable load magnify the recovered energy. In a seasonal or low-load facility, the same device may take longer to return.
Fuel price and boiler efficiency
The same heat recovery creates higher monetary value on expensive fuel. The lower calorific value of the fuel and the current boiler efficiency should be used in the savings calculation.
Too much air
Higher air quantity than necessary increases flue gas flow rate and loss. The economizer can recover some of this loss; but the root cause, the burner setting, must also be corrected.
Heat recovery calculation
Preliminary calculation can be made based on the heat lost by the flue gas or gained by the water:
Recovered heat = Water flow rate × Specific heat of water × Temperature increase
This value is multiplied by the operating time to find the annual energy. Boiler efficiency and fuel lower calorific value are taken into account when converting to fuel savings.
Annual monetary savings = Annual amount of fuel reduced × Fuel unit cost
Net savings are calculated after deducting pump/fan electricity, cleaning, maintenance and possible pressure loss expenses.
How is the payback period calculated?
Simple payback period = Total investment cost / Annual net savings
The total investment includes not only the economizer body. Bypass and damper, piping, pump, chimney modification, insulation, automation, transportation, installation and commissioning costs should also be added.
In long-term evaluation, it is more accurate to calculate cash flow for fuel price changes, maintenance, downtime and financing costs.
Why can’t flue gas be cooled indefinitely?
Sulfur in the fuel and combustion product water vapor can condense under certain temperatures and form acidic liquid. This can lead to rapid corrosion of the economizer and chimney. Safe outlet temperature should be determined by fuel composition, excess air, flue material and whether it is designed for condensing operation.
Using stainless materials alone does not solve all condensation risks. Condensate drainage, neutralization, surface temperature and chimney suitability should be examined together.
Things to consider on the water side
If the water starts to boil in the economizer, flow instability and vapor locking may occur. Flow, pressure and outlet temperature must be kept safe over the entire load range. The head of the boiler feed water pump must cover the economizer pressure loss.
Contact of cold oxygenated water with hot surfaces and improper water chemistry can increase corrosion. Water preparation, deaerator and chemical conditioning system should be evaluated as a whole.
Contamination in solid fuel systems
Ash and soot close the gap between the finned surfaces, reducing heat transfer and increasing gas side pressure loss. Pipe spacing should be selected appropriate to the ash content of the fuel, volatile matter, slagging tendency and particle load. Cleaning access and method must be defined in the project.
How to monitor economizer performance?
- Flue gas inlet and outlet temperature,
- Water inlet and outlet temperature,
- Water flow rate,
- Gas and water side pressure loss,
- Boiler load and fuel consumption,
- Flue gas oxygen value,
- Surface contamination and cleaning interval
It should be recorded regularly. Performance degradation can be detected early by referencing the initial commissioning values.
Frequently asked questions
How much percent does the economizer increase boiler efficiency?
There is no fixed rate. It should be calculated by measuring flue gas temperature, load, feed water, fuel and operating hours.
Can an economizer be installed later on the existing boiler?
Can be evaluated in most facilities; Chimney fan capacity, pressure loss, area, piping, automation and corrosion conditions should be checked.
Does the economizer rot the chimney?
Wrong temperature and material selection may cause acid condensation. Risk can be managed when the dew point and flue system suitable for the fuel are calculated.
Can domestic water be heated instead of feed water?
Different fluids can be evaluated with appropriate exchanger design; Consumption continuity, hygiene, pressure and corrosion conditions are determined according to the project.
Technical resources
- T.R. Ministry of Energy and Natural Resources, Energy Efficient Technologies in Industry.
- T.R. Ministry of Energy and Natural Resources, Energy Efficiency in Boilers training resources.